
 Phone
 Send Email
 whatsapp
 Facebook


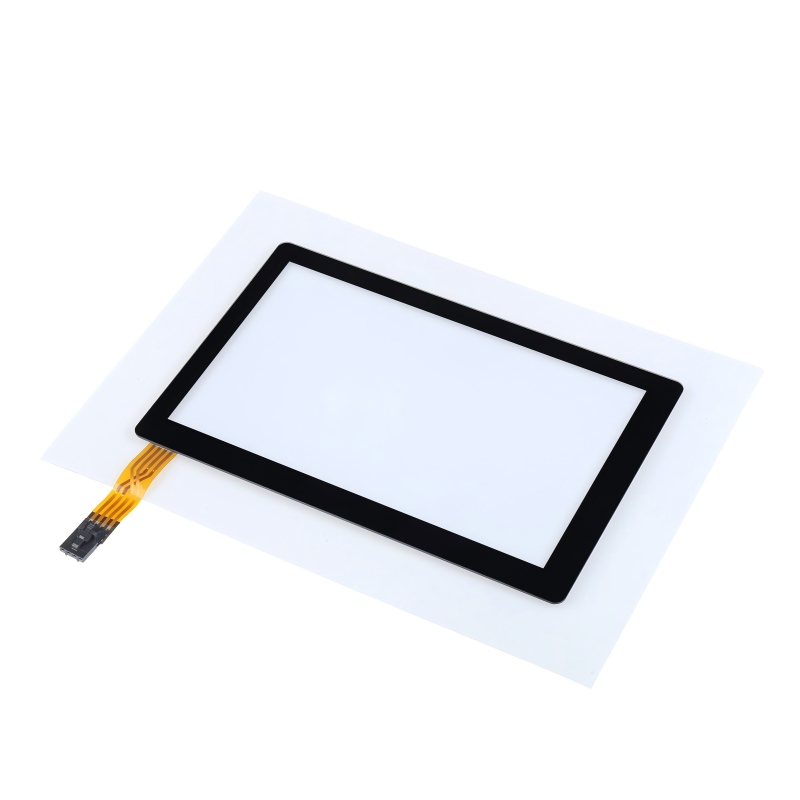


High-Temperature Screen-Printed ITO on Fused Quartz
Background
The client approached us with a transparent heating element project—a glass panel that would be electrically heated and used in an environment where both optical clarity and mechanical durability were critical. The original concept was built around borosilicate glass, with sputtered ITO as the transparent conductor, silver paste for the electrode termination, and a hard AR overcoat to protect the ITO from scratches during handling and installation. On paper, it looked like a straightforward build. The challenge emerged when we looked at the operating temperature: 350°C continuous. At that level, most standard Ar Coatings and conventional ITO stacks start to show signs of stress, and we knew early on that we would need to validate the entire material system before committing to production.
Customer Drawing Specifications
The following parameters were extracted directly from the customer's production drawing:
| Parameter | Specification |
|---|---|
| Part dimensions | 40 mm × 50 mm |
| Thickness | 5 mm |
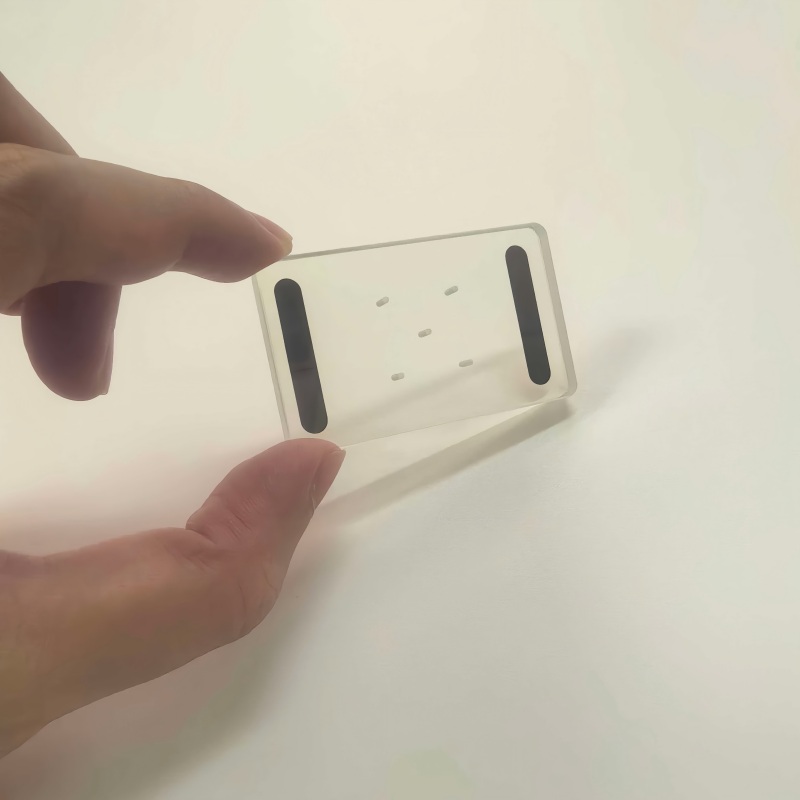
| Through-holes | 5 holes, φ1.0 mm each |
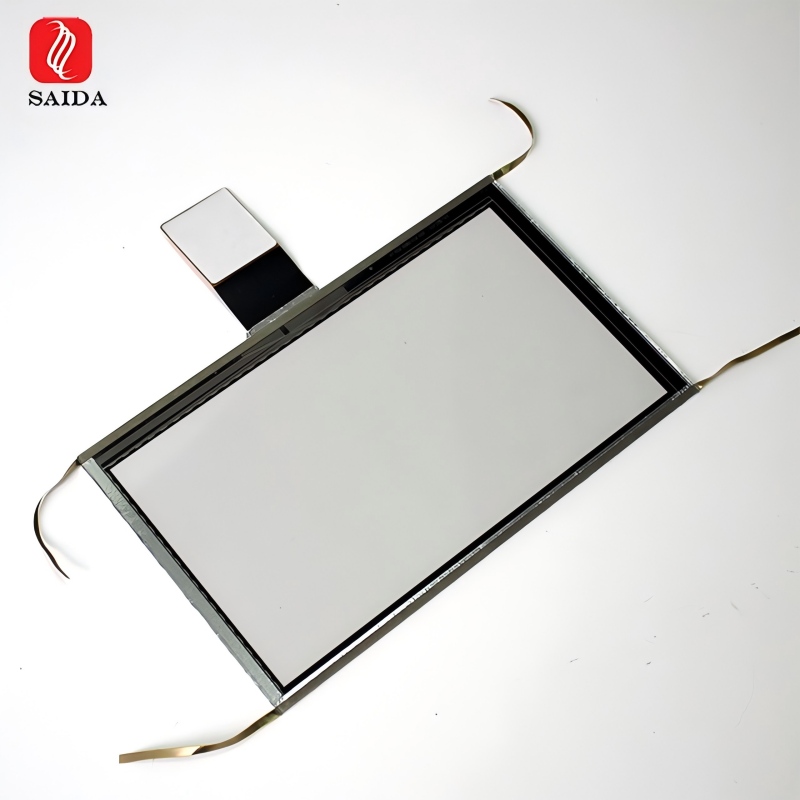
| Heating area | Defined by printed ITO pattern (see drawing) |
| Electrode layout | Copper paste traces as per drawing pattern |
| Electrical rating | 28 V / 2.5 A |
| Maximum operating temperature | 350°C |
| Resistance | 5-15 OHM |
| Transmittance | High transparency at 1050nm |
| Substrate | Borosilicate glass |
| Surface treatment | Super hard AR coating for anti scratch on ITO layer |
These specifications set the boundaries for our material selection and process development. Two items immediately stood out as critical: the 350°C thermal ceiling and the five 1 mm through-holes in borosilicate glass—a combination that would drive most of our engineering decisions.
Initial Testing and Failure Analysis
We built the first set of prototypes exactly to the original material specification: borosilicate substrate, sputtered ITO, copper paste electrodes, and a hard AR topcoat. Thermal cycling began at room temperature and ramped gradually to 350°C.
The AR coating was the first to fail. As temperature crossed the 300°C mark, we observed visible crazing and localized delamination. The root cause was identified as CTE mismatch: the AR material's expansion coefficient diverged from that of the underlying ITO layer, creating interfacial shear stress that exceeded the film's adhesion strength. By the time the surface reached 350°C, optical haze had risen above 8%, and the ITO's sheet resistance drifted upward by approximately 15% from its baseline value. The stack was thermally unstable and optically compromised—clearly not a viable path forward.
Material and Process Redesign
Based on the failure analysis, we proposed three fundamental changes:
| Aspect | Original Approach | Revised Approach |
|---|---|---|
| Substrate | Borosilicate glass (CTE: ~3.3×10⁻⁶/°C) | Fused quartz (CTE: ~0.5×10⁻⁶/°C) |
| ITO deposition | Sputtering | High-temperature screen-printing |
| Electrode | Standard copper paste | High-temperature silver paste formulation |
| AR overcoat | Hard AR layer | Eliminated entirely |
Why we dropped the AR layer: after high-temperature firing, the screen-printed ITO film develops a surface roughness of approximately 0.3 to 0.5 µm Ra. This inherent texture provides sufficient mechanical scratch resistance for ordinary handling, making a separate reinforced AR overcoat unnecessary. Removing that interface simplified the layer stack and, more importantly, eliminated the primary failure mechanism we observed during initial testing.
Manufacturing Challenge: The 1 mm Through-Holes
The five φ1.0 mm through-holes turned out to be the most demanding aspect of production. Fused quartz is hard (Vickers ~900–1000 HV) and brittle, with low fracture toughness. Standard drilling parameters would almost certainly induce edge chipping or micro-cracks, compromising both mechanical strength and the integrity of the surrounding conductive traces.
We developed a dedicated drilling protocol:
- Diamond-core drill bits with fine grit
- Stepped feed rate: 0.2 mm/s for initial contact (to prevent edge chipping), then 0.6 mm/s through the bulk
- Continuous water-based coolant to suppress localized heating and thermal shock
- Post-drilling inspection under magnification to verify edge quality
In parallel, we adjusted the screen-printing mask to ensure the ITO layer maintained a minimum clearance of 0.5 mm from each hole perimeter. This prevented conductive paste from wicking into the drilled edges during the firing stage, which could have created short circuits or non-uniform heating patterns.
Validation and Results
After successfully performing thermal cycling tests from ambient to 350°C, repeated over 200 cycles, the customer has now moved the design into pre-production validation, and we are confident the solution will hold up in the field.