In the crowded world of ITO glass, having solid CE certification really makes a difference. Richard Chen, who’s pretty much considered an expert in the field, says it best: “CE certification isn’t just some label; it’s a real promise of quality.” That really drives home how important it is to follow industry standards. When you buyIto Coated Glass from certified suppliers, you’re pretty much guaranteed safety and reliability. But, honestly, some suppliers don’t see the value in certification, which can cause all sorts of issues like inconsistent quality and unhappy customers. Building a good reputation in the Ito Glass market really comes down to trust and sticking to proven standards.
And let’s not forget, having top-notch CE certification can seriously boost your market appeal. Customers tend to go for suppliers who take compliance seriously. That said, getting certified isn’t always a walk in the park — it can be pretty complicated and pushy. If you don’t handle it right, you could lose out on some key clients. Knowing just how important certification is can really help suppliers stay competitive in this industry. Overall, it’s all about making sure everyone knows you’re serious about quality, and that really pays off in the long run.
Importance of CE Certification for Ito Glass Suppliers
CE certification holds great importance for suppliers of Ito glass. This certification ensures that products meet European safety and environmental standards. It acts as a reliable indicator of quality and compliance. Consumers and businesses prefer products that bear the CE mark, as it reflects a commitment to excellence.
Obtaining CE certification can be challenging. It requires extensive documentation and understanding of regulatory standards. Suppliers must invest time in meeting these requirements. Oversights can lead to delays in certification, impacting business operations. Suppliers often need to conduct thorough testing to affirm compliance. This process can feel overwhelming, but it strengthens product reliability.
Tip: Stay informed about evolving regulations to maintain compliance. Regular training can help your team understand the certification process. Building relationships with certification bodies can also facilitate smoother certification.
Tip: Consider periodic audits of your processes. This ensures that you remain compliant over time. Addressing potential issues early can prevent complications in the future. Regular assessments enhance product quality and customer trust.
Importance of CE Certification for Ito Glass Suppliers
Understanding the CE Marking Process and Requirements
The CE marking process is essential for Ito glass suppliers. It indicates that products meet European safety and health standards. Each requirement of the CE process must be understood and followed precisely. Failure to comply can lead to serious consequences, including product recalls and financial losses.
To start, suppliers must conduct a thorough risk assessment. This process identifies potential hazards associated with theIr Glass products. After this, they must gather appropriatetechnical documentation. This includes design specifications, material data, and manufacturing processes. Quite often, suppliers overlook this documentation, which can create issues during audits.
Finally, testing is a critical step. Independent laboratories verify that the products meet CE marking standards. However, many suppliers remain uncertain about testing processes and criteria. This uncertainty can cause delays in market entry. Ensuring clarity within these requirements, especially for Ito On Glass, is vital for success. Suppliers should seek expert advice to navigate this complex system. Engaging with knowledgeable professionals can bridge the gap in understanding.
Benefits of High-Quality CE Certification for Manufacturers
High-quality CE certification plays a crucial role for Ito glass suppliers. It not only ensures compliance with European standards but also enhances marketability. Many potential clients look for suppliers who can demonstrate such certifications. This can lead to increased trust and credibility in a competitive market.
Moreover, having high-quality CE certification often results in improved product safety and reliability. It provides manufacturers with a clear framework to assess and enhance their production processes. As a result, businesses can minimize the risk of defects and recalls. This focus on quality demonstrates a commitment to both consumer safety and industry standards.
However, achieving high-quality CE certification can be challenging. It requires rigorous testing and documentation. Some suppliers may struggle with the demands of the certification process. This presents an opportunity for reflection and growth. By addressing these challenges, suppliers can build their expertise and elevate their offerings in the long run.
Impact of CE Certification on Market Access and Competitiveness
High-quality CE certification plays a crucial role in enhancing market access for Ito glass suppliers. CE certification assures consumers and businesses that products meet specific safety and health standards set by the European Union. Research indicates that 90% of companies without CE marking face significant barriers in accessing EU markets. This underscores the importance for suppliers to acquire certification in today's competitive landscape.
For Ito Coated Glass Substrate suppliers, the implications are profound. Certified products can open doors to lucrative opportunities across Europe, increasing potential sales by up to 30%. However, achieving CE certification involves meticulous testing and compliance with rigorous standards. Many suppliers struggle with the complexities of this process. A lack of understanding can lead to setbacks, impacting market entry.
Moreover, the competitive edge gained from having CE certification can be lost if not maintained. Suppliers must stay abreast of changing regulations. Continuous investment in quality management systems is not just recommended; it's essential for sustained growth. Failure to adapt could result in losing market share as competitors capitalize on compliance.
Risks of Non-Compliance with CE Certification Standards
CE certification is essential for suppliers, particularly in the glass industry. The absence of compliance can lead to significant risks. For Ito Glass suppliers, failing to meet CE standards may result in unsafe products. This can damage reputation and customer trust. Non-compliance can even lead to legal liabilities. Regulatory bodies closely monitor the marketplace. They are vigilant about standards that ensure product safety and quality.
Moreover, the market demands high-quality products. Ito Glass Substrates are no exception. Customers expect durability and safety. If a supplier's products lack CE certification, they may face rejection in competitive bids. Buyers will likely favor certified options. This can lead to lost sales and weakened market position. In some cases, non-compliance may even lead to recalls. Such incidents can cost significant time and resources, impacting business longevity.
It's crucial for suppliers to invest in quality assurance. CE certification offers a framework for evaluating compliance. Suppliers should reflect on their practices and ensure they align with industry standards. The potential risks associated with non-compliance can outweigh the costs of adhering to CE certification. Ultimately, maintaining high standards is not just about meeting regulations; it's about fostering trust and ensuring safety for all stakeholders involved.
Role of Third-Party Testing in Achieving CE Certification
In an increasingly competitive market, achieving CE certification is crucial for Ito Glass suppliers. This certification demonstrates that products meet EU safety, health, and environmental standards. Third-party testing plays a vital role in this process. Independent labs assess the quality and safety of glass products, providing an unbiased evaluation that adds credibility.
A recent industry report reveals that 70% of suppliers who invest in third-party testing report higher customer confidence. Customers are more likely to trust products that have undergone rigorous testing. When Ito Glass Slides pass these assessments, they stand out in quality, enhancing brand reputation.
Tips: Consider regular testing as part of your production cycle. Implementing routine checks can help address potential issues early. Additionally, work with well-recognized testing facilities to ensure reliability. Even minor discrepancies in manufacturing can lead to significant compliance issues. Prioritizing consistent quality checks can turn challenges into advantages.
In the long run, the benefits of CE certification and third-party testing significantly outweigh the costs. However, many suppliers overlook the importance of these processes. Continuous engagement with testing can result in better compliance and market positioning. Adopting a proactive approach to quality assurance will not only enhance product safety but also align with consumer expectations.
Why High-Quality CE Certification Matters for Ito Glass Suppliers? - Role of Third-Party Testing in Achieving CE Certification
| Aspect | Importance | Benefits | Third-Party Testing Role |
| Product Compliance | Ensures safety and meets EU standards | Increases marketability across Europe | Validates compliance through unbiased reviews |
| Consumer Trust | Enhances consumer confidence in the product | Boosts sales and brand loyalty | Provides transparency in product testing |
| Regulatory Compliance | Avoids legal issues and fines | Encourages easier entry into new markets | Ensures adherence to all required standards |
| Quality Assurance | Guarantees the quality of products | Reduces returns and defects | Implements rigorous testing protocols |
| Market Demand | Increases competitiveness in the market | Captures wider consumer base | Provides data supporting product quality |
Future Trends in CE Certification for Glass Industry Suppliers
The landscape of CE certification is evolving rapidly for glass industry suppliers. With rising standards, transparency has become more crucial. Suppliers must stay updated with new regulations. This often requires additional training and investment in quality control systems. The complexity of compliance can be daunting. Many suppliers struggle to navigate these changes effectively, leading to delays in certification processes.
Sustainability is another pressing concern. As the industry shifts toward eco-friendly practices, CE certification will increasingly reflect these values. Suppliers that prioritize sustainable methods will enhance their reputations. However, achieving this often means reevaluating supply chains and production practices. Some may find it challenging to balance profitability with sustainability efforts. Inconsistencies in the adoption of these practices can impact overall certification quality.
Moreover, technology plays a pivotal role in CE certification’s future. Digital tools can streamline compliance processes, making it easier for suppliers to meet requirements. Yet, not every supplier is equipped with advanced technology. This disparity could result in varying levels of certification quality across the industry. Suppliers must be proactive. Keeping pace with technology and regulatory changes is essential for maintaining competitiveness. The path ahead is challenging, but it presents opportunities for those willing to adapt.
Innovative Coating Technologies: Enhancing Cover Glass with Anti-Reflective, Anti-Glare, and Anti-Fingerprint Features
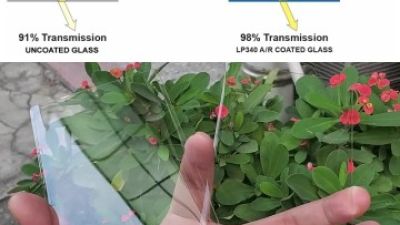
Innovative coating technologies have revolutionized the performance of cover glass in a variety of applications. By incorporating anti-reflective (AR), anti-glare (AG), and anti-fingerprint (AF) features, these specialized coatings significantly enhance the optical clarity and usability of cover glass. The AR coating minimizes reflections, allowing for better visibility in various lighting conditions, making it ideal for consumer electronics such as smartphones and tablets. This is particularly important in outdoor settings where bright sunlight can interfere with screen readability.
Similarly, anti-glare coatings are designed to reduce the harshness of reflections, providing a more comfortable viewing experience. This technology is crucial for automotive applications, where glare can distract drivers and pose safety risks. Furthermore, the integration of anti-fingerprint features ensures that the glass surface remains clean and smudge-free, enhancing both durability and aesthetic appeal. These coatings not only improve user experience but also extend the lifespan of the cover glass, reducing the need for frequent replacements.
The application process for these coatings requires precise parameters to ensure optimal performance. Factors such as thickness, adhesion, and chemical composition must be meticulously controlled to achieve the desired effects. As industries continue to adapt to demands for high-quality, functional materials, the development and implementation of these innovative coating technologies will play a pivotal role in advancing cover glass solutions across diverse fields.
FAQS
: CE certification indicates compliance with European safety and environmental standards. It assures quality and reliability.
It boosts marketability and consumer trust. Products with CE marks are preferred by businesses and customers alike.
Suppliers must provide extensive documentation and undergo rigorous testing. Oversights can delay certification, affecting operations.
Regular training and maintaining relationships with certification bodies can help suppliers stay informed about evolving regulations.
Independent labs assess product safety and quality, providing an unbiased evaluation that enhances credibility and customer confidence.
Periodic audits help identify potential compliance issues early. Addressing these can prevent future complications and improve product quality.
It minimizes defect risks and recalls, demonstrating a commitment to consumer safety and industry standards over time.
Keeping consistent quality checks and engaging in regular testing can enhance compliance and market positioning over time.
Addressing difficulties can lead to growth, helping suppliers build expertise and elevate product offerings in competitive markets.
Conclusion
High-quality CE certification is crucial for Ito Glass suppliers as it ensures compliance with European regulatory standards, enhancing product safety and marketability. The CE marking process requires manufacturers to meet specific requirements, which can significantly influence their competitive position in the market. Suppliers who invest in high-quality certification benefit from increased market access and consumer trust, ultimately leading to greater business opportunities.
Moreover, the risks of non-compliance with CE certification standards can be severe, potentially resulting in legal repercussions and loss of market share. Third-party testing plays a vital role in helping Ito Glass manufacturers attain certification by providing an unbiased verification of product quality. As the glass industry evolves, staying informed about future trends in CE certification will be essential for suppliers looking to maintain their competitive edge and ensure the safety and reliability of their products.

 Phone
 Send Email
 whatsapp
 Facebook